

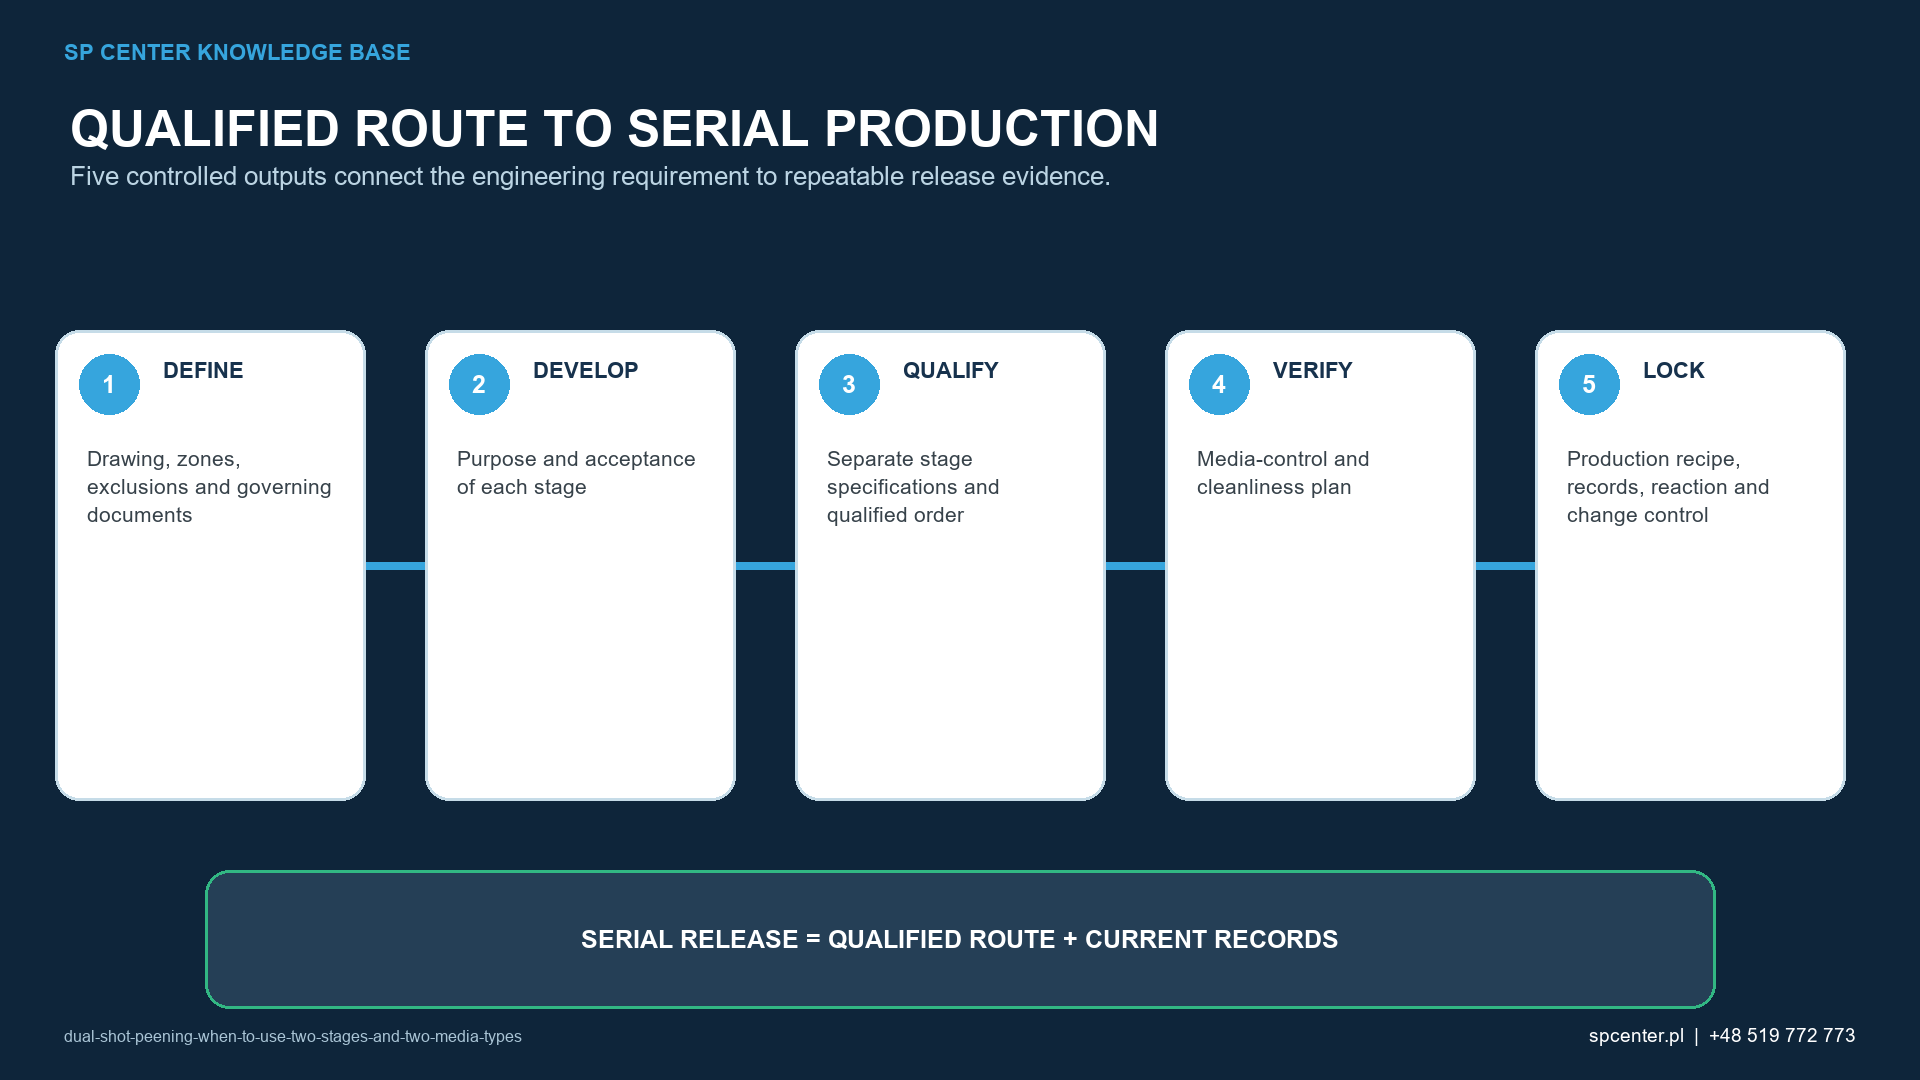
Define two ordered stages, separate media and Almen controls, coverage, transition cleanliness, combined validation and linked batch records
Dual shot peening is not simply a longer cycle. It is an intentionally specified sequence of two separately controlled peening stages, often with different media or process levels. The first stage can establish one part of the required surface and residual-stress response, while the second modifies the near-surface condition. The order, media, intensity, coverage, treatment zones, transition and combined acceptance must be qualified; a claimed benefit cannot be inferred from the phrase dual peening alone.
What makes a process dual shot peening?
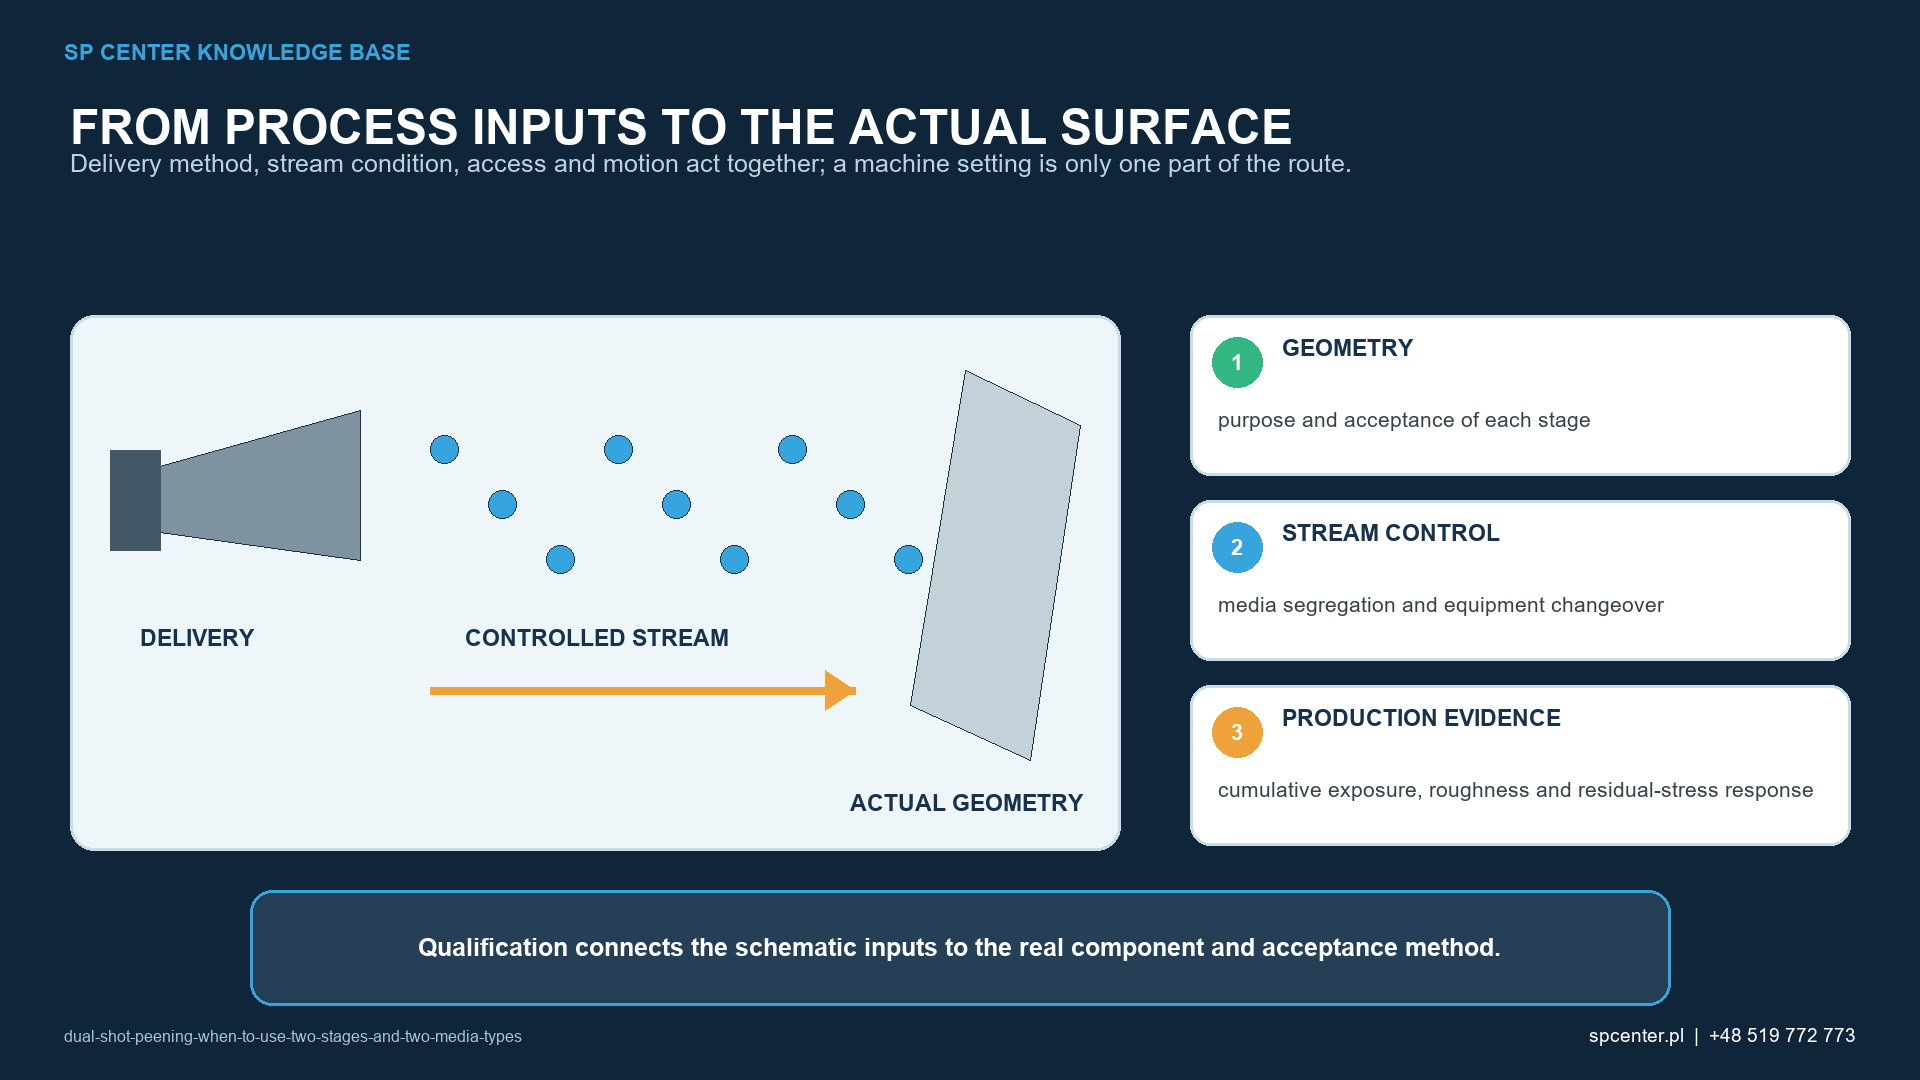
A two-stage route identifies stage 1 and stage 2 as distinct controlled operations. Each has defined equipment, media, Almen intensity where invoked, coverage, fixture, masks, motion and exposure. The route also defines the allowed condition between stages and the final acceptance after both are complete.
An extra pass with the same settings, a restart after an interruption or a repair cycle is not automatically dual shot peening. Those events follow the approved exposure, reprocessing and nonconformance rules of the governing documents.
Why might two stages be specified?
| Development objective | Possible two-stage concept | Boundary that must be proved |
|---|---|---|
| Residual-stress depth plus near-surface condition | A first stage develops the primary stress field; a second controlled stage modifies the near-surface response | The second stage must not erase, overwork or destabilize the required first-stage result |
| Roughness or surface texture | A finer medium may be evaluated after a coarser first stage | A smoother average reading is not guaranteed and does not prove fatigue or stress depth |
| Coverage of difficult texture | Two defined impact populations can be evaluated on the same treatment zone | Neither stage compensates for shadowing, leakage or an inaccessible feature |
| Material-specific surface response | Media materials, sizes, hardnesses and energies are selected for the exact alloy and condition | Contamination, embedding, folding, cracking and dimensional limits remain acceptable |
| Legacy or customer-defined route | The drawing or process specification invokes two ordered stages | Supplier changes require formal authority; order and ranges are not optional |
| Component performance | The combined route is validated against a single-stage baseline when required | Benefits remain bounded by the tested material, geometry, load and environment |
Table 1. A two-stage route needs a specific engineering objective and evidence that the combined result remains acceptable.
A common development concept is to use the first stage for the principal residual-stress depth and the second for a finer near-surface response. This is a concept, not a universal recipe. Depending on material and settings, the second stage can change roughness, cold work, maximum compressive stress, surface stress, dimensions or damage risk in ways that require measurement.
How is dual peening different from 100% or 200% coverage?
Coverage is the proportion of a required surface showing impact evidence under the approved inspection method. When the governing requirement defines 200% coverage through exposure time, it generally means twice the total time needed to establish 100% coverage for that process configuration.
Dual peening instead uses two separately defined impact populations. Each stage can have its own coverage requirement. Two stages do not automatically equal 200%, and 200% with one medium does not create a qualified dual route.
How should the two media be selected?
Media selection considers component material and heat treatment, required stress profile, surface and contamination limits, feature size, edge sensitivity, roughness, distortion and equipment capability. Type, nominal size, hardness, shape and operating condition are all controlled. Finer second-stage media is common in some routes but is not mandatory unless the design basis requires it.
Changing only media size can also change impact energy, coverage rate, rebound, retention and measurement response. A designation is therefore not a substitute for separate qualification of each complete stage.
Why are cleaning and media segregation critical?
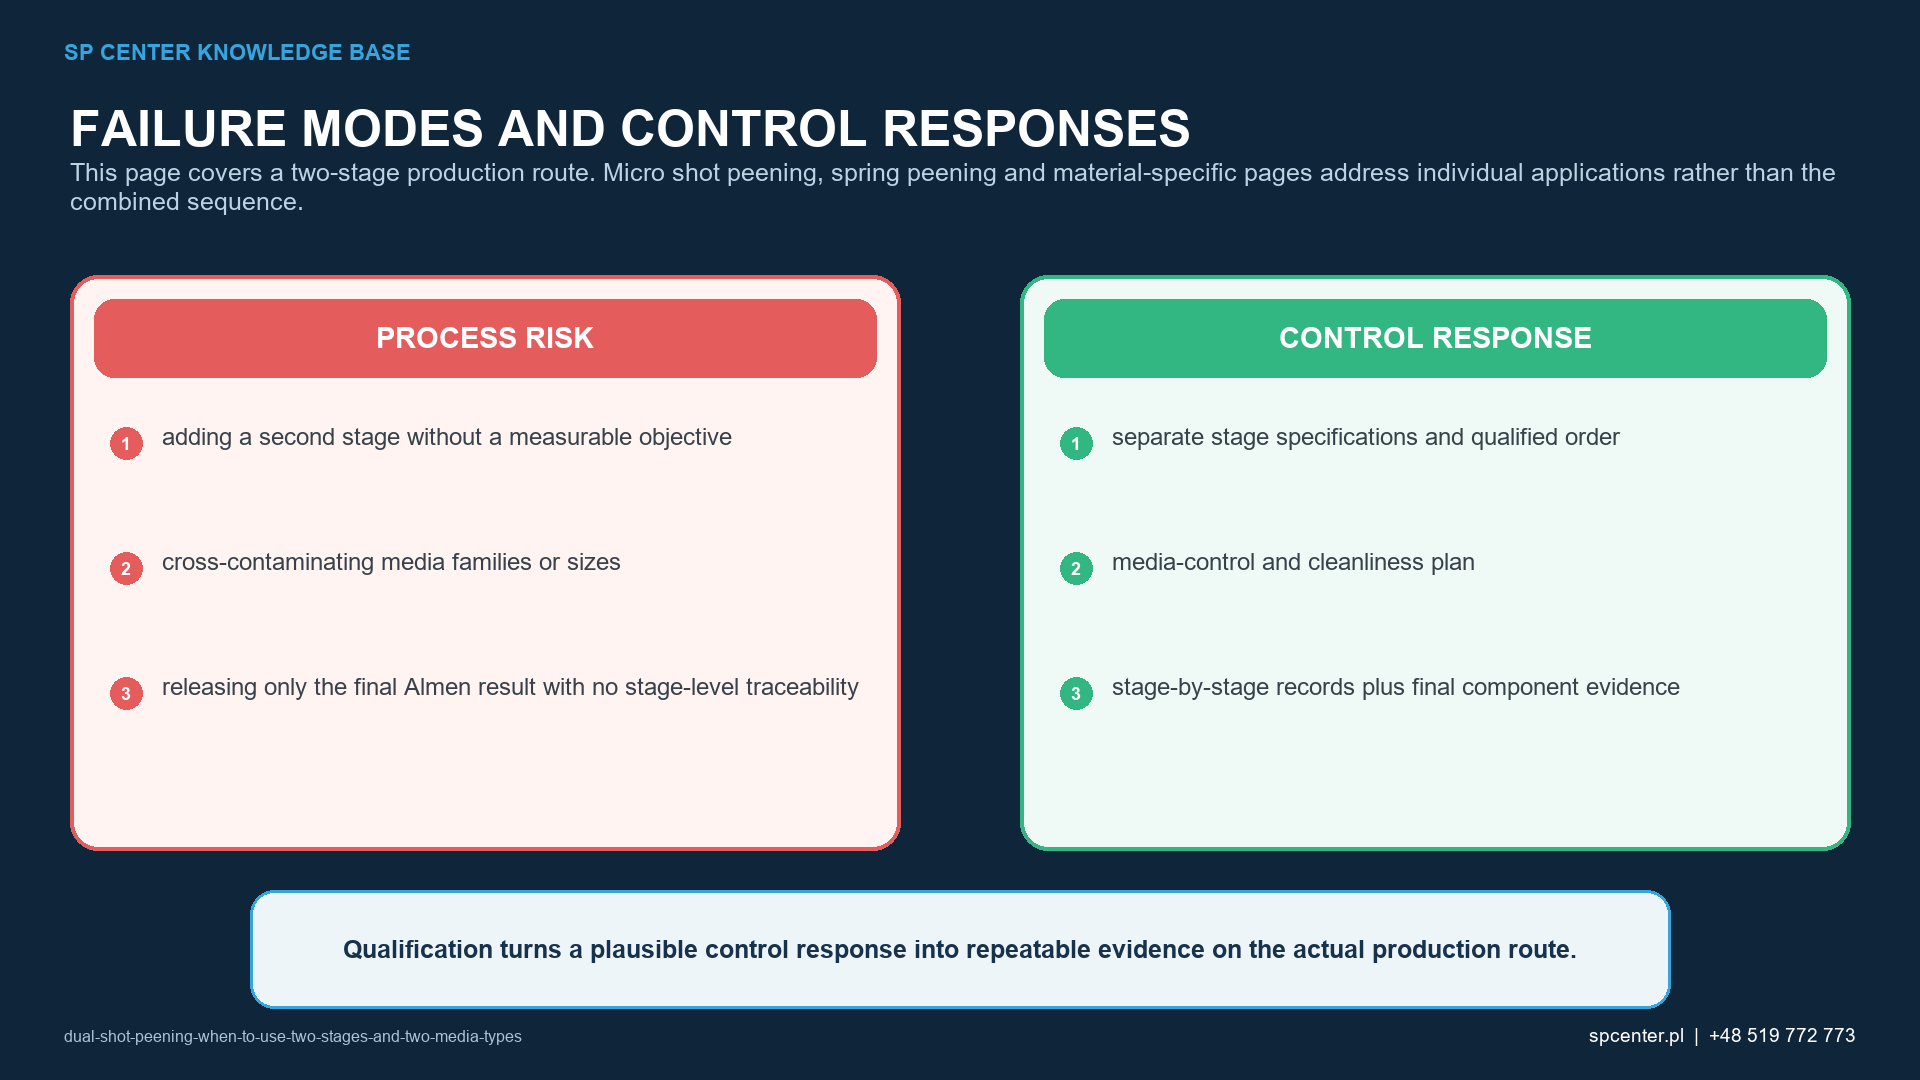
Carryover can change the impact population of the second stage or introduce material incompatible with a component’s contamination restrictions. Media can remain in bores, masks, fixtures, pockets, containers or handling equipment. Merely changing the machine label or emptying a visible hopper does not prove segregation.
The qualified route should define dedicated circuits or validated cleaning, shot recovery, container identity, inspection and allowable transition condition. If stages occur at different sites or times, preservation, part status and traceability must remain controlled.
How is each stage qualified?
| Qualification item | Stage 1 | Stage 2 and combined result |
|---|---|---|
| Process identity | Equipment, programme, fixture, masks, media circuit and treatment zones | Equipment, programme, fixture, masks, media circuit, treatment zones and fixed sequence |
| Media | Type, designation, size, hardness, shape, contamination and operating condition | Separate type and designation plus evidence that transfer from stage 1 is controlled |
| Intensity | Complete Almen range, strip designation, saturation-curve basis and verification arrangement | Its own complete Almen range, strip designation, saturation-curve basis and verification arrangement |
| Coverage | Required coverage and approved inspection conditions for every stage-1 zone | Required stage-2 coverage plus acceptance of final boundaries and surface |
| Part condition | Incoming material, heat treatment, prior operations, cleanliness, damage and dimensions | Allowed transition condition, final roughness, damage, cleanliness, dimensions and retained media |
| Validation | Baseline surface and residual-stress evidence when invoked | Combined residual-stress profile, fatigue or other application evidence when invoked |
Table 2. Stage-specific intensity and coverage evidence lead to a separate combined component result.
Where Almen intensity is invoked, each stage requires its specified range, strip designation, holder arrangement and saturation-curve basis. Pressure, wheel speed or a stage-1 correlation must not replace stage-2 verification. Coverage is assessed on the actual required zones for that stage.
The final surface can require roughness, visual damage, boundary, cleanliness, retained-media and dimensional checks. Residual-stress depth or fatigue testing can be used during validation when the design authority invokes it; neither is automatically a routine batch-release test.
Does the order of the stages matter?
Yes. Reversing the stages changes which impact population acts on the final surface and can alter roughness, stress profile, cold work and damage risk. Order is part of the qualified process identity, not an operator preference.
Delay, cleaning, storage or another manufacturing operation between stages can also affect the part condition. The route should state what is allowed and when a repeated intensity or surface verification is needed.
What can invalidate the combined result?
- Wrong stage order, medium, intensity range, coverage or treatment map.
- Open failure or missing records from stage 1.
- Media carryover, mixed lots or unverified cleaning between stages.
- Fixture, mask or motion change that alters access or boundaries.
- Uncontrolled interruption, partial restart or extra exposure.
- Roughness, damage, dimensions, cleanliness or retained media outside the final limits.
- Process change transferred from another part without authorization and qualification.
What should be recorded for every batch?
| Production record | Minimum traceability | Stop condition |
|---|---|---|
| Part and route | Part, lot, drawing revision, material condition and two-stage process revision | Wrong or incomplete process identity |
| Stage 1 | Machine, programme, fixture, masks, media, Almen evidence, coverage, exposure and alarms | Open nonconformance or missing evidence before stage 2 |
| Transition | Time or holding condition when relevant, cleaning, media removal, transfer identification and protection | Unknown stage status, mixed lots or uncontrolled contamination |
| Stage 2 | Machine, programme, fixture, masks, media, Almen evidence, coverage, exposure and alarms | Wrong medium, order, settings or treatment zone |
| Final acceptance | Surface, boundaries, roughness, damage, dimensions, cleanliness and retained-media checks as invoked | Result outside any drawing or process limit |
| Release | Deviations, dispositions, customer forms, certificate and authorized approval | Open deviation, undocumented rework or incomplete linked record |
Table 3. Stage 1, transition, stage 2 and final release must form one traceable evidence chain.
What information belongs in an RFQ?
- Current drawing, revision, part and specification hierarchy.
- Material, heat treatment, hardness, prior operations and incoming surface.
- Separate stage-1 and stage-2 treatment and exclusion zones.
- Media type, designation, size, hardness and contamination limits for both stages.
- Complete Almen range and strip designation plus coverage for each stage.
- Allowed interval, cleaning, handling and preservation between stages.
- Final surface, roughness, dimensional, residual-stress or fatigue evidence as invoked.
- Source approval, qualification, records, lot pattern, packaging and delivery target.
Frequently asked questions
What is dual shot peening?
Dual shot peening is an intentionally specified sequence of two separately controlled peening stages. Each stage can use a different medium, Almen intensity, coverage and configuration. The combined route must be qualified as a whole.
Is dual shot peening the same as 200% coverage?
No. Two hundred percent coverage normally refers to total exposure equal to twice the time required to establish 100% coverage when the governing requirement defines it that way. Dual peening uses two distinct process stages.
Must the second stage use smaller media?
Not as a universal rule. A finer or different medium is common in some developed routes, but media, order, intensity and coverage must come from the drawing, specification or approved qualification.
Does the second stage always improve surface roughness?
No. Surface response depends on both media, energies, material, incoming texture, angle and exposure. Roughness must be measured with the approved method and remains separate from residual-stress and fatigue evidence.
Does each stage need an Almen saturation curve?
Each stage needs the intensity evidence required by the governing route. Where Almen intensity is invoked, do not assume the curve or machine setting from one stage represents the other.
Can a failed first stage be accepted after the second stage passes?
No automatic recovery is valid. A second stage cannot close an open nonconformance or reconstruct missing evidence. The part must be contained and dispositioned under authorized procedures.
How is media cross-contamination controlled?
Use segregated circuits or validated cleaning and transfer controls, identified containers, condition checks and documented limits appropriate to both media and the component material.
When should dual shot peening be selected?
Only when the design or process authority has a defined engineering objective and the two-stage route demonstrates the required surface, dimensional, residual-stress or fatigue outcome better than or differently from an approved single-stage route.
Key takeaways
- Dual shot peening is two qualified stages, not simply twice the exposure.
- Each stage needs its own media, intensity, coverage and configuration evidence.
- Stage order and the transition condition are controlled characteristics.
- Media segregation and complete removal protect both process control and the component.
- The final combined result needs surface, dimensional and application evidence as invoked.
- A second stage cannot silently repair an open first-stage nonconformance.
Related SP Center guides
- 100% vs 200% Shot Peening Coverage
- Media Contamination in Shot Peening
- Residual-Stress Depth Profiles
Technical references
1. SAE AMS2430U: Shot Peening, revised April 2018
2. SAE AMS2432E: Shot Peening, Computer Monitored, revised October 2022
3. SAE AMS2431E: Peening Media, General Requirements, revised April 2023
4. SAE ARP7488: Peening Design and Process Control Guidelines, issued January 2018
5. SAE J442_202602: Tools for Peening Intensity Determination and Verification, revised February 2026
6. SAE J443_202512: Procedures for Determining and Verifying Peening Intensity, revised December 2025
7. SAE J2277_202301: Shot Peening Coverage Determination, revised January 2023
Standards note: No two-stage sequence should be inferred from a public abstract. The complete revisions, drawing and customer-specific requirements invoked by the contract govern.
Author: Paweł Kmieć
Discuss a two-stage shot peening requirement: +48 519 772 773 | [email protected]